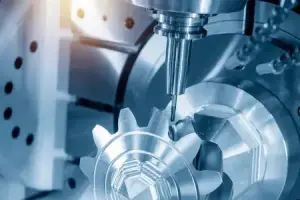

A robotic cnc cell looks like a six-axis arm holding a spindle, and on a shop floor it draws every visitor's eye. It is not, however, a smaller version of a machining center. A robot arm mills large patterns, molds, and foam blocks where a three-axis VMC would struggle to reach, but it cannot hold a ±0.01 mm tolerance on a hardened-steel bracket the way a machining center does. A boat-builder in Croatia once tried to replace a five-axis CNC with a robotic cnc setup for making hull plugs; the surface came out fine on the foam pattern, but when they asked the cell to trim a carbon-fiber layup to ±0.2 mm the arm flexed and the part had to be hand-finished. This guide walks a pattern shop, a foundry, or an end-user automating a deburring cell through six checks to run before you order robotic cnc machining: work envelope, repeatability, material, spindle power, offline programming, and the cases where you should skip the arm and stick to a machining center.
1. Work Envelope and Reach
The robot arm's reach defines the largest part you can put on the table. A 2 m reach arm sounds generous until you mount the spindle, add the tool length, and realize the cutting envelope shrinks by 300 mm on every side. Measure the longest dimension of your pattern, mold, or fixture, then add the tool length and the spindle nose. A robotic cnc cell that just barely reaches the corner of a 1.8 m foam block will chatter at the wrist limit every cycle, and that chatter shows up as tool marks on the pattern. If the part needs to be flipped and re-fixtured for the second side, plan two setups up front rather than asking one arm to reach around the corner.
2. Precision and Repeatability
Robot arms repeat to about ±0.05 to ±0.1 mm, while a machining center holds ±0.01 mm or better. That is enough for foam, wood, expanded polystyrene, and most sculpted patterns, but it is not enough for precision-machined metal features. Ask the supplier whether the ±0.05 mm number is the arm's bare-body repeatability or a measured cutting repeatability under load; the two can differ by a factor of two. A robotic cnc cell quoted at ±0.05 mm that drifts to ±0.15 mm under a 5 Nm cut will leave a visible step on a carbon-fiber trim path. Ask for a sample cut on your material before you sign the PO; a 30-minute trial cut costs less than reworking a rejected pattern.
3. Material Type and Removal Rate
Robotic cnc cells earn their keep on soft, large-form materials: foam, wood, wax, foam patterns for foundry, clay, and low-density foamed tooling board. They can cut aluminum and engineering plastics, but the material removal rate is a fraction of a machining center because the arm flexes under load. If your job is trimming a carbon-fiber molding or deburring a casting, the arm is a good fit; if it is hogging out a solid aluminum mold to near-net shape, a machining center will finish the job in a quarter of the time. Sand casting patterns, foam plugs, and sculpted EPS are the sweet spot where the arm's flexibility beats a fixed spindle.
4. Spindle Power and Tooling
The spindle bolted to the wrist is what actually cuts. Entry-level robotic cnc cells ship with 1 to 3 kW spindles for foam and wood; a cell expected to trim carbon fiber or aluminum needs 6 to 12 kW and an HSK or ER40 holder. Check the tool change: a robotic cnc cell with a manual tool change every 30 minutes will lose more time than it saves, while a 12-tool automatic changer costs as much as the arm itself. For one-off pattern work, manual changes are fine; for a recurring trim job, budget for the changer from day one.
5. Offline Programming and CAM
Robot arms do not read G-code the way a machining center does. They need offline programming software, a CAM post that maps tool paths to joint angles, and a collision check before the first cut. If your shop programs machining centers in Fusion 360 or Mastercam, ask the supplier whether the post processor is included or sold separately. A robotic cnc cell without a proven post will sit idle for the first month while someone figures out how to send a tool path to the wrist. Budget a two-week commissioning window and a day of offline programming training for the operator who will run the cell.
6. When to Skip Robotic CNC
Robotic cnc is the wrong answer for small precision parts, hardened-steel hard milling, high-volume production runs, and any job where the tolerance is tighter than ±0.05 mm. If the part fits inside a 600 mm cube and needs to be metal, a machining center is faster, more accurate, and often cheaper per part. The arm wins on size, access, and automation of repetitive trim or deburring tasks; it does not win on absolute precision.
Run these six checks and the robotic cnc cell you order will fit your largest pattern, hold the tolerance your material actually needs, and come with a spindle and tool change that match your cycle time. Start with work envelope and repeatability, then work out the spindle power and offline programming before you compare price. For related background, read our automotive cnc machining materials guide and our precision cnc milling service page before you shortlist; when the quotes come back, cross-check the prototype scope in our functional plastic prototypes page and the small-batch capability in our brass cnc milling page, so the first install does not turn into a rework order.